 ,
Xu Chun-cheng,
Cui Zhou-bo,
Zhu Yi-shi,
Wu Lin-rui,
Wang Yao-de,
Wang Yan,
Gao Wei-kang
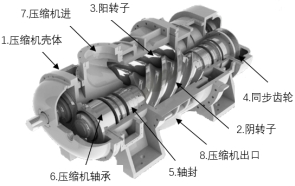
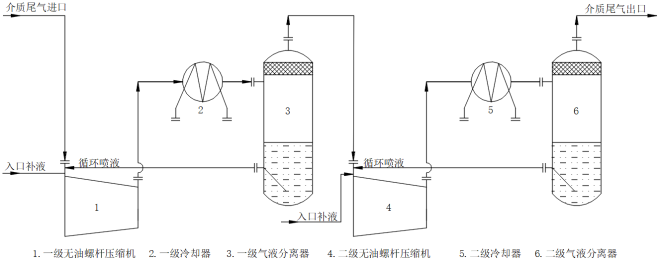
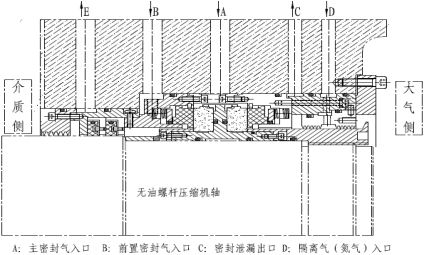
Aiming at the difficult to recover hydrogen chloride mixed tail gas generated during the production of lithium bis(fluorosulfonyl)imide (LiFSI), the PRO II process simulation software was adopted to optimize the parameters of the compression condensation recovery process in this paper. Considering equipment investment, operating energy consumption and anti corrosion risks comprehensively, the optimal process parameters were determined, with the final compressor pressure of 2.0MPaG and condensation recovery temperature of 0°C. By comparing the advantages and disadvantages of reciprocating compressors and oil injected screw compressors, a two stage series oil free screw compressor was selected as the pressurization equipment. High temperature corrosion caused by acidic gas was inhibited by upgrading the compressor casing and rotor to 2205 duplex steel material and using thionyl chloride as the special internal liquid spraying medium. A three stage composite sealing structure consisting of front labyrinth, double end dry gas and isolation comb tooth seals was designed to achieve zero leakage of process gas. The industrial operation results of the LG58/0.0 2.0 unit show that under working conditions with wide fluctuations of inlet pressure (0–0.01MPaG) and inlet temperature (−10–10°C), the discharge pressure of the unit remains stable, the outlet temperature can be steadily controlled within 70–75°C, no medium leakage or oil contamination occurs, and the purity of recovered hydrogen chloride products meets process requirements. This complete oil free screw compression solution can provide engineering references for pressurization recovery and equipment selection of strongly corrosive mixed gas in the lithium battery and fluorine chemical industries.
| Published in | Science Research (Volume 14, Issue 5) |
| DOI | 10.11648/j.sr.20261405.22 |
| Page(s) | 350-355 |
| Creative Commons |
This is an Open Access article, distributed under the terms of the Creative Commons Attribution 4.0 International License (http://creativecommons.org/licenses/by/4.0/), which permits unrestricted use, distribution and reproduction in any medium or format, provided the original work is properly cited. |
| Copyright |
Copyright © The Author(s), 2026. Published by Science Publishing Group |
Oil-free Screw Compressor, Hydrogen Chloride Mixed Gas, Gas Compression, Condensation Recovery
序号 | 名称 | 单位 | 数据 |
|---|---|---|---|
1 | 温度 | °C | 0 |
2 | 压力 | MPaG | 0 |
3 | 组分 | Mol% | HCl (60%), SO2 (35%), SOCL2 (5%) |
序号 | 冷凝压力/MPaG | 冷凝温度/°C | 压缩电耗/kWh | 循环水/t/h | 制冷电耗/kWh | 回收率/% |
|---|---|---|---|---|---|---|
1 | 0.5 | -40 | 300 | 32 | 594 | 100 |
2 | 1.0 | -20 | 400 | 51 | 356 | 100 |
3 | 1.5 | -10 | 470 | 75 | 206 | 100 |
4 | 2.0 | 0 | 521 | 95 | 109 | 100 |
5 | 2.5 | 5 | 563 | 112 | 66 | 100 |
序号 | 级数 | 1级 | 2级 |
|---|---|---|---|
1 | 压缩机入口压力(MPaG) | 0 | - |
2 | 压缩机入口温度(°C) | 0 | 40 |
3 | 压缩机出口压力(MPaG) | 0.93 | 2.03 |
4 | 压缩机出口温度(°C) | 85 | 85 |
5 | 冷却器后压力(MPaG) | 0.9 | 2.0 |
6 | 冷却器后温度(°C) | 40 | 40 |
序号 | 项目 | 设计工况 | 运行工况 |
|---|---|---|---|
1 | 一级入口压力(MPaG) | 0 | 0~0.01 |
2 | 一级入口温度(°C) | 0 | -10~10 |
3 | 一级出口压力(MPaG) | 0.93 | 0.92 |
4 | 一级出口温度(°C) | 85 | 70~75 |
5 | 一级冷却器后压力(MPaG) | 0.93 | 0.9 |
6 | 一级冷却器后温度(°C) | 40 | 40 |
7 | 一级喷液量(t/h) | 3.3 | 4.5~5.6 |
8 | 二级出口压力(MPaG) | 2.03 | 2.03 |
9 | 二级出口温度(°C) | 85 | 70~75 |
10 | 二级冷却器压力(MPaG) | 2.0 | 2.0 |
11 | 冷却器后温度(°C) | 40 | 40 |
12 | 二级喷液量(t/h) | 1.7 | 2.2~3.0 |
| [1] | 刘剑锋, 干式螺杆压缩机在芳烃干气压缩中的研究与应用 [J]. 2014, (04): 22-25. |
| [2] | 马文静, 徐延学, 周全, 崔周波. 无油螺杆压缩机在煤制乙二醇低压排放气回收的研究与应用 [J]. 石油化工设备技术, 2021, 42(4): 40. |
| [3] | 肖芳, 马文静, 李敏. 喷油工艺螺杆压缩机的特点及应用分 析. 现代化工 [J]. 2012, 32(10): 87. |
| [4] | 舒丹丹, 许子通, 徐春成, 李敏. 入口节流在螺杆压缩机启动过程中的应用研究 [J]. 2026, (02): 7-10. |
| [5] | 张照坡, 张梦蕾, 李亚楠. 双氟磺酰亚胺锂的合成 [J]. 2024, 41(08): 18-20. |
| [6] | 刘宇宁, 马德龙, 马松, 王德楼, 董玉灿, 王才朋, 冉升亮 [J]. 2023, 52(1): 77-79. |
| [7] | 李倩慧, 张亚, 郑丹丹,李亚楠, 孙永明, 李富斌, 薛峰峰. 双氟磺酰亚胺锂的性能及其在锂离子电池中的应用[J]. 2020, 37: 10. |
| [8] | 邢子文. 螺杆压缩机—理论、设计及应用 [M]. 北京: 机械工业出版社, 2003. |
| [9] | 陈彪, 王辰. C4热泵精馏压缩机选型.石油化工设备技术 [J], 2020, 41(6). |
| [10] | 丁兆亮, 沈冬明, 金轩轾, 无油螺杆压缩机干气系统的应用 [J]. 2023, (06): 35-38. |
| [11] | 袁浩, 唐昊, 何志龙, 邢子文. 喷液冷却的两级无油螺杆氨气压缩机性能研究. 设计研究 [J]. 2014, 05. |
| [12] | 蔡宏, 范年宝. 工艺用无油螺杆压缩机的结构与设计. 流体机械 [J]. 2011, 39(10): 50. |
| [13] | 马林, 胡涛, 连小松, 蔡宏. 无油螺杆压缩机在液氨精制回收中研究与应用. 应用与测试 [J]. 2013, (01): 53-56. |
| [14] | 魏希超, 压缩机干气密封泄漏分析与处理经验[J]. 2024, 53(01): 75-79. |
| [15] | 刘剑锋, 干式螺杆压缩机在芳烃干气压缩中的研究与应用[J]. 2014, (04): 22-25. |
APA Style
You-cai, W., Chun-cheng, X., Zhou-bo, C., Yi-shi, Z., Lin-rui, W., et al. (2026). Application of Oil-free Screw Compressor in Hydrogen Chloride Mixed Gas Compression. Science Research, 14(5), 350-355. https://doi.org/10.11648/j.sr.20261405.22
ACS Style
You-cai, W.; Chun-cheng, X.; Zhou-bo, C.; Yi-shi, Z.; Lin-rui, W., et al. Application of Oil-free Screw Compressor in Hydrogen Chloride Mixed Gas Compression. Sci. Res. 2026, 14(5), 350-355. doi: 10.11648/j.sr.20261405.22
AMA Style
You-cai W, Chun-cheng X, Zhou-bo C, Yi-shi Z, Lin-rui W, et al. Application of Oil-free Screw Compressor in Hydrogen Chloride Mixed Gas Compression. Sci Res. 2026;14(5):350-355. doi: 10.11648/j.sr.20261405.22
@article{10.11648/j.sr.20261405.22,
  author = {Wang You-cai and Xu Chun-cheng and Cui Zhou-bo and Zhu Yi-shi and Wu Lin-rui and Wang Yao-de and Wang Yan and Gao Wei-kang},
  title = {Application of Oil-free Screw Compressor in Hydrogen Chloride Mixed Gas Compression},
  journal = {Science Research},
  volume = {14},
  number = {5},
  pages = {350-355},
  doi = {10.11648/j.sr.20261405.22},
  url = {https://doi.org/10.11648/j.sr.20261405.22},
  eprint = {https://article.sciencepublishinggroup.com/pdf/10.11648.j.sr.20261405.22},
  abstract = {Aiming at the difficult to recover hydrogen chloride mixed tail gas generated during the production of lithium bis(fluorosulfonyl)imide (LiFSI), the PRO II process simulation software was adopted to optimize the parameters of the compression condensation recovery process in this paper. Considering equipment investment, operating energy consumption and anti corrosion risks comprehensively, the optimal process parameters were determined, with the final compressor pressure of 2.0MPaG and condensation recovery temperature of 0°C. By comparing the advantages and disadvantages of reciprocating compressors and oil injected screw compressors, a two stage series oil free screw compressor was selected as the pressurization equipment. High temperature corrosion caused by acidic gas was inhibited by upgrading the compressor casing and rotor to 2205 duplex steel material and using thionyl chloride as the special internal liquid spraying medium. A three stage composite sealing structure consisting of front labyrinth, double end dry gas and isolation comb tooth seals was designed to achieve zero leakage of process gas. The industrial operation results of the LG58/0.0 2.0 unit show that under working conditions with wide fluctuations of inlet pressure (0–0.01MPaG) and inlet temperature (−10–10°C), the discharge pressure of the unit remains stable, the outlet temperature can be steadily controlled within 70–75°C, no medium leakage or oil contamination occurs, and the purity of recovered hydrogen chloride products meets process requirements. This complete oil free screw compression solution can provide engineering references for pressurization recovery and equipment selection of strongly corrosive mixed gas in the lithium battery and fluorine chemical industries.},
 year = {2026}
}
TY  - JOUR
T1  - Application of Oil-free Screw Compressor in Hydrogen Chloride Mixed Gas Compression
AU  - Wang You-cai
AU  - Xu Chun-cheng
AU  - Cui Zhou-bo
AU  - Zhu Yi-shi
AU  - Wu Lin-rui
AU  - Wang Yao-de
AU  - Wang Yan
AU  - Gao Wei-kang
Y1  - 2026/09/14
PY  - 2026
N1  - https://doi.org/10.11648/j.sr.20261405.22
DO  - 10.11648/j.sr.20261405.22
T2  - Science Research
JF  - Science Research
JO  - Science Research
SP  - 350
EP  - 355
PB  - Science Publishing Group
SN  - 2329-0927
UR  - https://doi.org/10.11648/j.sr.20261405.22
AB  - Aiming at the difficult to recover hydrogen chloride mixed tail gas generated during the production of lithium bis(fluorosulfonyl)imide (LiFSI), the PRO II process simulation software was adopted to optimize the parameters of the compression condensation recovery process in this paper. Considering equipment investment, operating energy consumption and anti corrosion risks comprehensively, the optimal process parameters were determined, with the final compressor pressure of 2.0MPaG and condensation recovery temperature of 0°C. By comparing the advantages and disadvantages of reciprocating compressors and oil injected screw compressors, a two stage series oil free screw compressor was selected as the pressurization equipment. High temperature corrosion caused by acidic gas was inhibited by upgrading the compressor casing and rotor to 2205 duplex steel material and using thionyl chloride as the special internal liquid spraying medium. A three stage composite sealing structure consisting of front labyrinth, double end dry gas and isolation comb tooth seals was designed to achieve zero leakage of process gas. The industrial operation results of the LG58/0.0 2.0 unit show that under working conditions with wide fluctuations of inlet pressure (0–0.01MPaG) and inlet temperature (−10–10°C), the discharge pressure of the unit remains stable, the outlet temperature can be steadily controlled within 70–75°C, no medium leakage or oil contamination occurs, and the purity of recovered hydrogen chloride products meets process requirements. This complete oil free screw compression solution can provide engineering references for pressurization recovery and equipment selection of strongly corrosive mixed gas in the lithium battery and fluorine chemical industries.
VL  - 14
IS  - 5
ER  -
Technical Department,Shanghai Marine Diesel Engine Research Institute, Shanghai, China
Technical Department,Shanghai Marine Diesel Engine Research Institute, Shanghai, China
Technical Department,Shanghai Marine Diesel Engine Research Institute, Shanghai, China
Technical Department,Shanghai Marine Diesel Engine Research Institute, Shanghai, China
Technical Department,Shanghai Marine Diesel Engine Research Institute, Shanghai, China
Technical Department,Shanghai Marine Diesel Engine Research Institute, Shanghai, China
Technical Department,Shanghai Marine Diesel Engine Research Institute, Shanghai, China
Technical Department,Shanghai Marine Diesel Engine Research Institute, Shanghai, China
Information

 Share This Article
 Twitter
 Linked In
 Facebook

 Copy
 Download